Contact our Global Team
Choosing China’s best vitamins manufacturers requires more than comparing prices or attractive packaging. Buyers need evidence of formulation expertise, production consistency, and responsible quality control. This guide examines suppliers producing Vitamins To Boost Immune System products for private-label brands, distributors, and healthcare businesses.
Experienced manufacturers should explain their ingredient sources, dosage rationale, and stability testing. They should also provide batch records, certificates of analysis, and clear allergen information. Facilities following recognized GMP and food-safety systems offer a stronger foundation for reliable production. However, certification alone does not prove every product performs equally well. Independent laboratory testing still matters.
A dependable supplier should communicate clearly before a contract is signed. Ask about minimum order quantities, lead times, packaging options, and recall procedures. Traceability should reach from raw materials to finished bottles. Product claims must remain accurate and suitable for the target market’s regulations. This is where practical judgment becomes important.
No supplier is perfect.
Some factories may present polished websites but provide limited technical evidence. Others may have excellent laboratories but weaker communication. Careful buyers should compare samples, audit reports, testing methods, and customer references. A responsible manufacturer will discuss formulation limits rather than promise dramatic immune benefits. Results can vary between individuals, and supplements should not replace balanced nutrition or professional medical advice. This introduction sets a practical basis for identifying credible Chinese partners with dependable standards, transparent documentation, and realistic expectations.
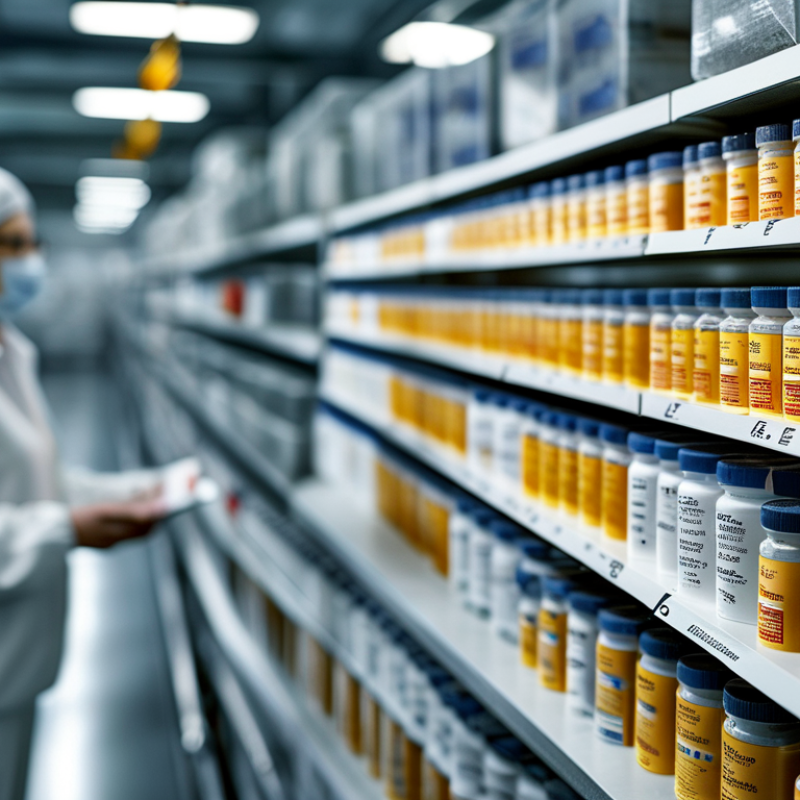
A reliable vitamin manufacturer in China should prove quality through controlled processes, not attractive promises. A polished website proves little. Ask for current manufacturing certifications, documented quality procedures, and clear production records. Responsible facilities can explain how raw materials are received, tested, stored, and released.
Independent laboratory testing also matters. Each batch should have a certificate of analysis covering identity, strength, purity, and microbiological safety. Traceability should connect the finished bottle to its ingredients, operators, equipment, and production date. During an audit, inspect cleaning records, calibration logs, warehouse conditions, and sample retention practices. Small details often reveal real discipline.
Technical experience is equally important. A capable team can discuss dosage forms, stability testing, moisture control, packaging compatibility, and flavor protection. They should also understand the destination market’s labeling and safety requirements. Clear communication reduces costly mistakes. Ask how they handle complaints, deviations, recalls, and delayed test results. Their answers should be specific, not rehearsed.
No factory is perfect. Even experienced manufacturers can face variability in materials or equipment. What matters is honest reporting and effective corrective action. Request pilot samples and compare them with later batches. Check whether the formula, color, texture, and testing results remain consistent. Reliability grows from evidence, transparency, and repeated performance. Convenience alone should not decide the partnership.
China Best Vitamins to Boost Immune System Manufacturers
Key Vitamins and Nutrients for Supporting Immune Health
Immune health depends on several nutrients, not one powerful ingredient. Vitamin C supports normal immune cell activity and helps protect cells from oxidative stress. Citrus fruits, peppers, and leafy vegetables provide useful food sources. Vitamin D also matters, especially for people with limited sunlight exposure. However, dosage should reflect laboratory results, age, and medical guidance.
Zinc supports immune signaling and helps maintain healthy skin barriers. Selenium contributes to antioxidant protection, while vitamin A supports the body’s mucosal defenses. Vitamins B6, B12, and folate assist normal blood and immune-cell formation. More is not always better. Excess vitamin A, zinc, or selenium may create health risks.
For manufacturers in China, reliable production should include identity testing, accurate dosage checks, stability studies, and contaminant screening. Clear certificates of analysis improve trust. GMP-based facilities and traceable raw materials matter. From a practical formulation view, combining nutrients is not automatically superior. Poor balance can reduce tolerability or create unnecessary intake. This deserves closer review. Individual needs also vary with diet, age, medication use, and existing conditions. A qualified healthcare professional should review high-dose products, particularly during pregnancy or chronic illness. Supplements should support a nutritious diet, not quietly replace it.
Chinese vitamin manufacturers are moving from basic contract production toward evidence-led immune-support products. Grand View Research valued the global dietary supplements market at about USD 177.5 billion in 2023, increasing pressure for reliable testing and clearer claims. Development usually begins with ingredient selection, dosage review, and target-user analysis. Manufacturers compare Chinese national standards, international monographs, and published clinical evidence before setting specifications.
The laboratory stage is practical. Each raw-material batch may undergo identity testing, potency analysis, microbial screening, and checks for heavy metals, pesticides, and moisture. Finished capsules or tablets are then tested for uniformity and dissolution. Stability studies place samples under heat and humidity, similar to warehouse conditions in southern China. Some facilities use ISO 22000 food-safety systems and GMP-based procedures, while independent laboratories verify selected results. Documentation matters.
Claims require restraint. The NIH Office of Dietary Supplements states that vitamins support normal immune function, but they do not guarantee disease prevention. This distinction should shape packaging and product design. A responsible manufacturer tracks supplier changes, keeps retained samples, and investigates unexpected results instead of hiding them. Not every formula deserves a launch.
There is room for improvement. Some testing programs still focus more on final products than on long-term consumer outcomes. Stronger post-market monitoring, transparent certificates, and well-designed human studies would make Chinese vitamin manufacturing more credible. For buyers, traceable batches and accessible test records are more meaningful than attractive immunity language.
China Best Vitamins to Boost Immune System Manufacturers
Quality Standards, Certifications, and Production Capabilities
Choosing a vitamin manufacturer requires more than comparing prices. Quality begins with documented Good Manufacturing Practice systems and trained production teams. Reliable facilities control raw materials, water quality, air conditions, and equipment sanitation. ISO 22000 or HACCP systems can strengthen food safety management. However, certification alone does not prove consistent product quality. Buyers should verify certificate scope, issuing bodies, and current validity.
Experienced manufacturers provide complete batch records and traceable ingredient codes. Each shipment should include a clear certificate of analysis, test methods, and specification limits. Independent laboratories can confirm vitamin strength, heavy metals, microbes, and common contaminants. Stability testing also matters, especially for sensitive powders and liquid formulas. I have found that practical sampling plans reveal more than attractive factory photographs. Sometimes, records are incomplete. That deserves careful questioning.
Production capability should match the intended product, volume, and market requirements. Facilities may offer blending, tablet compression, capsule filling, powder sachets, liquid filling, and controlled packaging. Separate allergen areas can reduce cross-contact risks. Validated cleaning procedures support safer changeovers between batches. Manufacturers should explain minimum order quantities, pilot production, lead times, and capacity during peak seasons. A thoughtful supplier also welcomes audits and corrective-action reviews. Small gaps can become serious problems. Regular communication remains essential.
| Evaluation Dimension | Relevant Standard or Capability | Verifiable Requirements | Why It Matters for Immune-Support Vitamin Products |
|---|---|---|---|
| Quality Management System | ISO 9001:2015 | A current certificate should identify the legal manufacturing site, certified scope, certification body, issue date, and expiry date. | Supports documented procedures, corrective actions, supplier control, complaint handling, and continuous improvement. |
| Food Safety Management | ISO 22000:2018 | The system should cover hazard analysis, prerequisite programs, operational controls, communication, verification, and emergency response. | Helps control biological, chemical, and physical hazards throughout vitamin and supplement production. |
| GFSI-Recognized Certification | FSSC 22000 or BRCGS Food Safety | Confirm the certificate is valid, site-specific, within scope, and supported by an accredited or officially recognized certification process. | Provides additional food-safety controls that are often requested by international retailers and importers. |
| HACCP Implementation | Codex HACCP principles | The manufacturer should maintain a documented hazard analysis, critical control points, monitoring limits, verification records, and corrective actions. | Reduces contamination and process risks for powders, tablets, capsules, gummies, and liquid formulations. |
| Good Manufacturing Practice | Market-specific dietary supplement or food-supplement GMP | The site should demonstrate controlled weighing, batch records, sanitation, personnel hygiene, deviation management, release procedures, and record retention. | Improves consistency of dosage, identity, purity, labeling, packaging, and batch release. |
| Laboratory Competence | ISO/IEC 17025 testing laboratory | Testing should use validated or verified methods, calibrated equipment, reference standards, documented uncertainty where applicable, and traceable reports. | Makes potency and contaminant results more reliable for export and regulatory review. |
| Raw-Material Identity | Identity testing and supplier qualification | Each incoming vitamin, mineral, botanical, excipient, and packaging component should be approved against specifications and linked to a supplier lot. | Helps prevent substitution, misidentification, adulteration, and formulation errors. |
| Potency and Content Uniformity | Assay testing and in-process controls | Finished products should be tested against approved specifications for declared nutrients such as vitamin C, vitamin D, vitamin A, vitamin B6, vitamin B12, zinc, or selenium. | Confirms that each batch delivers the declared nutrient amount within the applicable specification and tolerance. |
| Contaminant Control | Microbiological, heavy-metal, pesticide, solvent, and adulterant testing | The test panel should be based on ingredients, formulation, destination-market regulations, and identified risks. | Protects consumers from contamination risks that may occur in raw materials or during processing. |
| Dosage-Form Production | Tablets, hard capsules, powders, sachets, gummies, and liquid formats | Production equipment should be suitable for the selected format and supported by validated cleaning, changeover, weighing, filling, compression, or molding procedures. | Allows the same nutrient concept to be adapted for different consumer preferences and market requirements. |
| Cross-Contamination Prevention | Zoning, line clearance, validated sanitation, and allergen controls | The facility should separate or effectively control allergenic, high-risk, dusty, colored, and potent materials. | Reduces the chance of unintended carryover between vitamin and supplement batches. |
| Traceability and Recall | Lot coding and one-step-forward/one-step-back traceability | Raw materials, packaging, processing records, finished goods, and distribution documents should be linked by batch or lot number. | Enables rapid investigation and targeted withdrawal if a quality or safety issue is identified. |
| Stability and Shelf Life | Real-time and/or accelerated stability studies | Studies should consider temperature, humidity, packaging configuration, nutrient degradation, microbiological quality, and product appearance. | Supports scientifically justified expiry dates and storage instructions. |
| Packaging and Label Control | Controlled artwork approval and packaging inspection | Labels should be checked for ingredient declarations, serving size, allergen information, lot number, expiry date, storage conditions, and destination-market requirements. | Prevents labeling mistakes and helps ensure regulatory compliance in the target market. |
| Export and Documentation Readiness | Certificate of analysis, product specifications, batch records, and regulatory documents | A qualified manufacturer should be able to provide controlled technical files and product-specific documents without unexplained inconsistencies. | Simplifies importer qualification, customs review, customer audits, and product registration where required. |
Selecting a Chinese immune support manufacturer requires more than comparing prices. Review its production experience, quality systems, and export history. A reliable supplier should provide current GMP documentation, facility certificates, and product specifications. Ask for batch records, ingredient sources, and recent laboratory reports. Check whether independent laboratories verify identity, purity, microbiological safety, and heavy metals.
Request samples from the same production line used for commercial orders. Inspect the tablets, capsules, or powders for color, odor, texture, and packaging consistency. A professional manufacturer should explain its testing process clearly. It should also provide a certificate of analysis for every batch. Traceability matters. Each lot should connect to raw materials, production dates, operators, and test results.
Look closely at communication. Technical answers should arrive with evidence, not vague promises. Confirm minimum order quantities, lead times, storage conditions, and packaging options in writing. Review stability data for the intended market and check whether labels follow local regulations. Claims about immune support require careful wording. Overstated benefits can create serious compliance problems.
No audit is perfect. I have seen attractive facilities with weak documentation. A polished sample proves little. Arrange a video inspection or independent factory audit when possible. Small pilot orders can reveal delays, inconsistent packaging, or slow corrective actions. The best partner is not always the cheapest. It is the manufacturer that reports problems early and improves its process visibly.